Sep 8, 2026Design & Manufacturing
Silicone-to-Plastic Bonding: What Product Designers Should Check
Silicone-to-plastic overmolding can improve grip, sealing, cushioning and product integration. The main challenge is that not every plastic bonds to silicone in the same...
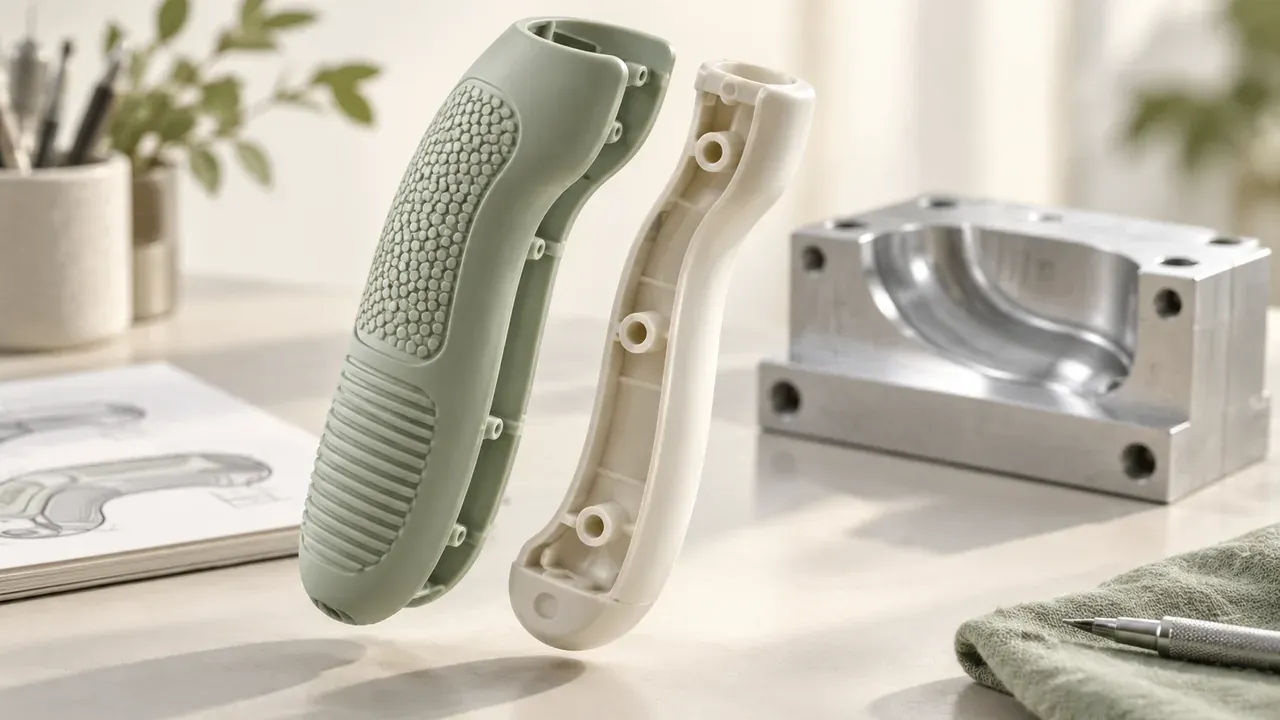
Silicone-to-plastic overmolding can improve grip, sealing, cushioning and product integration. The main challenge is that not every plastic bonds to silicone in the same way.
The design should not assume that silicone will stick to plastic simply because the geometry looks compatible.
Start with the plastic grade
Common engineering plastics used in overmolding projects may include PC, ABS, PA, PBT, PPS and other engineered resin grades. But the exact resin grade, additives, surface finish and heat history matter.
Check process-temperature compatibility
The plastic insert must remain dimensionally stable during molding. Potential problems include warpage, softening, local deformation and loss of dimensional fit.
Choose the bonding route deliberately
Silicone-to-plastic bonding may rely on direct chemical bonding, primer-assisted bonding, surface activation or mechanical locking. Mechanical locking can be useful when chemical bonding is uncertain or when the geometry allows retention features.
Watch the bond edge
Sealing performance on bonded assemblies
When a silicone seal is molded directly onto a plastic housing, the bond and the seal work as one system. Sealing performance still depends on the fundamentals: enough compression to close the leakage path without over-compression, a groove geometry that prevents rolling or extrusion, a hardness that suits the mating surface, and tolerance stack-up across both the silicone part and the rigid housing.
On overmolded seals, bond-edge lifting and insert deformation are the failure modes specific to the bonded construction, so seal geometry should be reviewed during DFM together with the tool design - flash, venting and local dimensions are all determined by the mold.
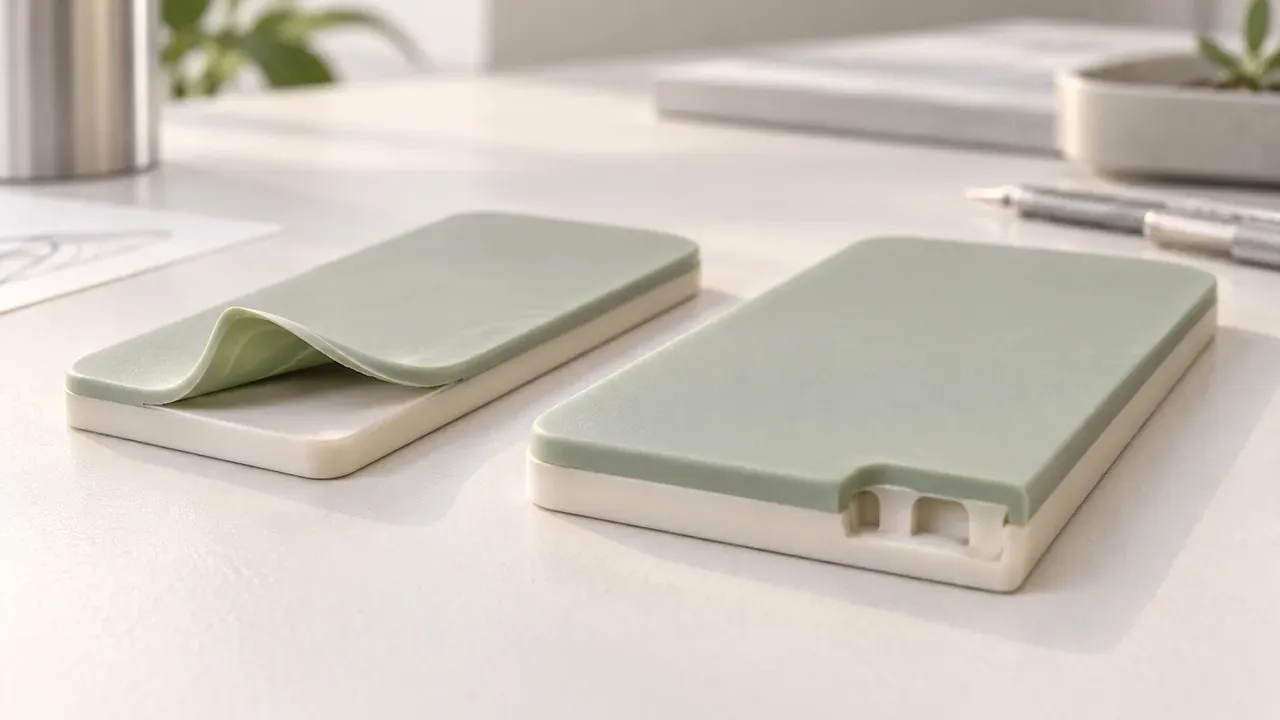
The edge of the bond is often where failures start. If the geometry allows the silicone edge to be repeatedly peeled or flexed, the interface may lift even if the center of the bond remains strong.
Surface cleanliness matters
Release agents, oils, dust and handling contamination can reduce bond consistency. This is why bonding performance should be treated as a manufacturing system, not only as a material choice.
Common failure modes
delamination
local lifting
flash
insert distortion
incomplete fill
poor edge definition
DFM questions to ask
Is chemical bonding required?
Can mechanical retention be added?
Can the insert tolerate molding temperature?
Can the insert be located repeatably?
Are the shut-off areas stable?
Is the bond edge exposed to peel forces?
Developing a silicone + plastic part? Send the substrate details and drawing for review.
Seeing these bonding issues in your own parts? The Functional & Overmolded Components group on our Electronics & Functional Components page shows the structures we build, and the Overmolding section under Capabilities explains the controls behind them.